
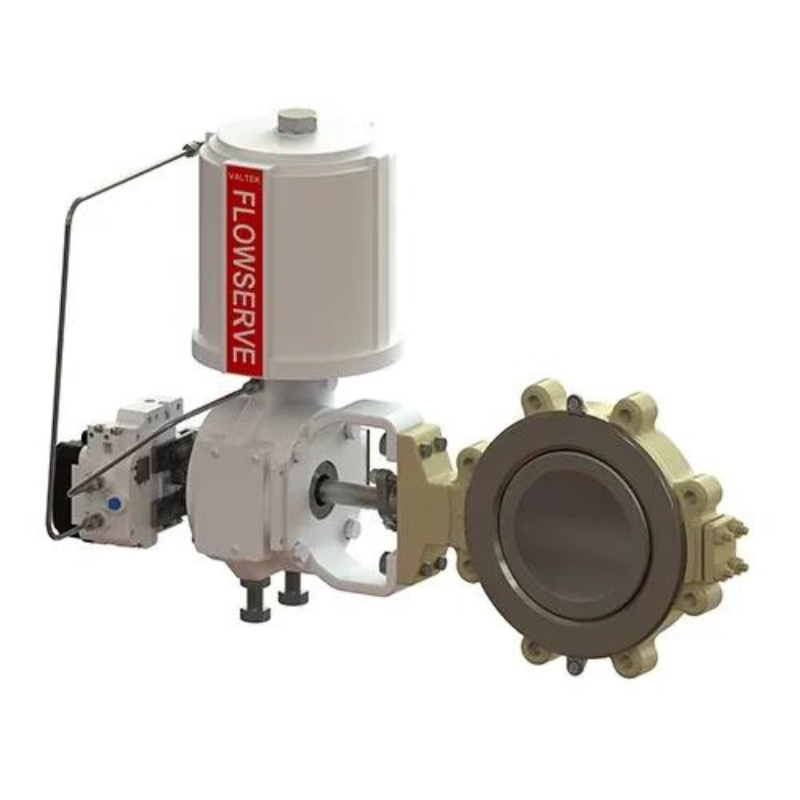
Control Valves
Introducing our advanced Mining Control Valves, the ultimate solution for optimizing and maintaining precise control in mining operations. Designed specifically for the demanding and rugged conditions of the mining industry, these valves offer exceptional performance, durability, and reliability, ensuring uninterrupted operation in the harshest environments.
Our Mining Control Valves are engineered to regulate the flow of various fluids, including water, slurry, chemicals, and gases, throughout the mining process. Whether it’s controlling the flow of water for dust suppression, managing the movement of slurry in pipelines, or regulating the flow of chemicals in mineral extraction, these valves provide unparalleled control accuracy and efficiency.
Choose our Mining Control Valves to optimize your mining processes, improve productivity, and ensure reliable and precise flow control. With their rugged construction, superior performance, and easy maintenance, these valves are the ideal choice for mining operations seeking unparalleled control and operational efficiency.
Key Features:
- Robust Construction: These valves are built to withstand extreme conditions, such as high pressures, abrasive materials, and temperature variations. Constructed from heavy-duty materials, they are resistant to corrosion, erosion, and wear, ensuring long-lasting performance even in the most challenging mining environments.
- Precise Flow Control: Our Mining Control Valves offer precise and responsive flow control, allowing operators to adjust the flow rates with precision. This level of control ensures optimal process efficiency, minimizes wastage, and enhances productivity, resulting in significant cost savings.
- Versatile Functionality: With a range of valve types available, including gate valves, globe valves, ball valves, and butterfly valves, our product line caters to diverse mining applications. Whether it’s regulating flow, isolating pipelines, or providing emergency shut-off capabilities, our valves are engineered to meet specific operational requirements.
- Easy Maintenance: We understand the importance of minimizing downtime in mining operations. Our valves are designed for easy maintenance, featuring accessible internal components and simplified maintenance procedures. This reduces maintenance time, enhances operational efficiency, and keeps your mining processes running smoothly.
- Enhanced Safety: Safety is a top priority in mining operations, and our control valves are designed with safety features in mind. They incorporate fail-safe mechanisms, such as emergency shut-off options, to prevent accidents and protect personnel and equipment from potential hazards.
- Compatibility and Integration: Our Mining Control Valves are compatible with industry-standard control systems, making integration into existing mining infrastructure seamless. They can be easily incorporated into automated systems, allowing for remote monitoring and control, further enhancing operational efficiency and safety.
Enquiry Form
"*" indicates required fields